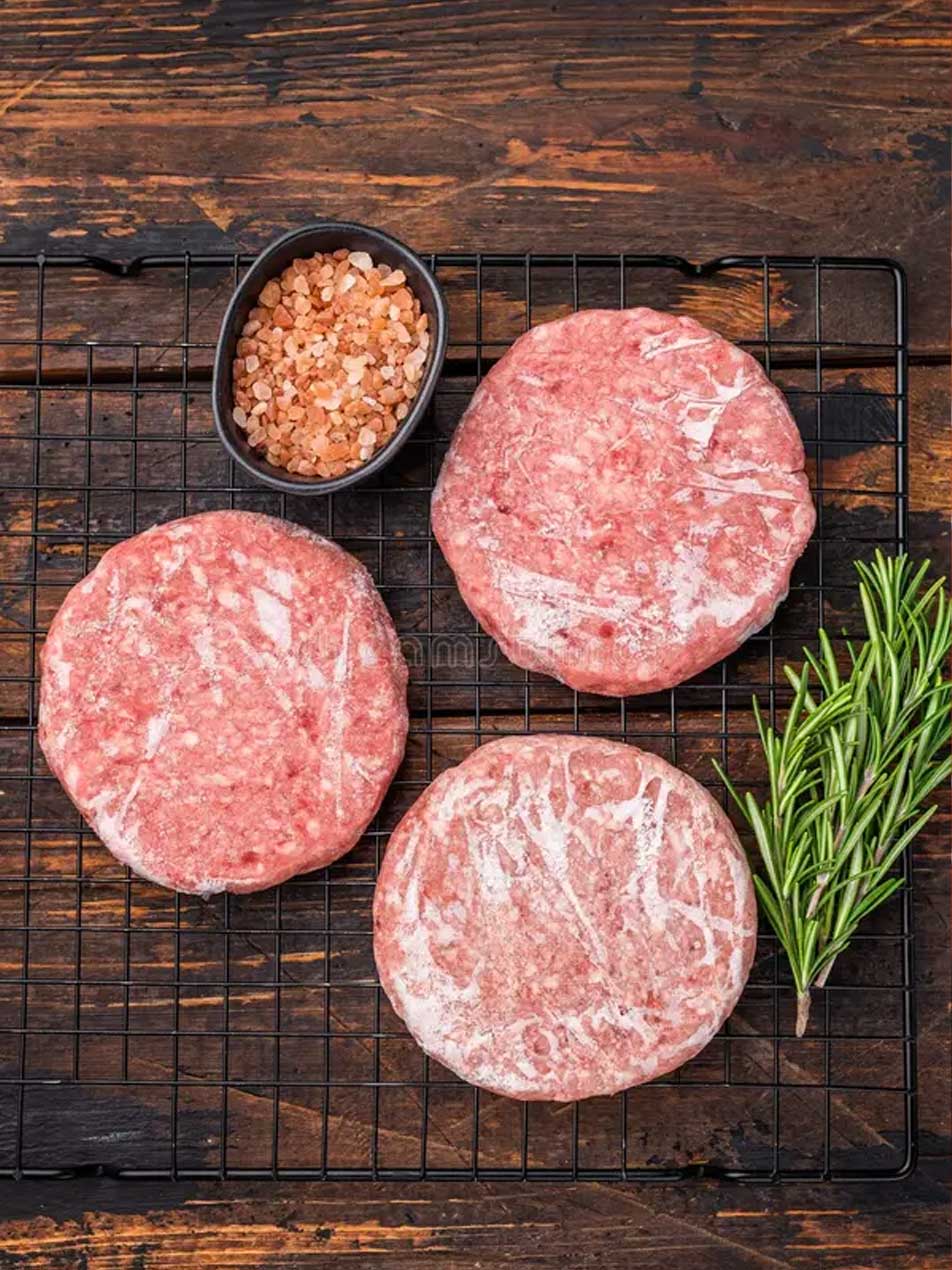
Packaged meat
Freezes boxed meat and poultry products uniformly while protecting carton shape and package integrity.

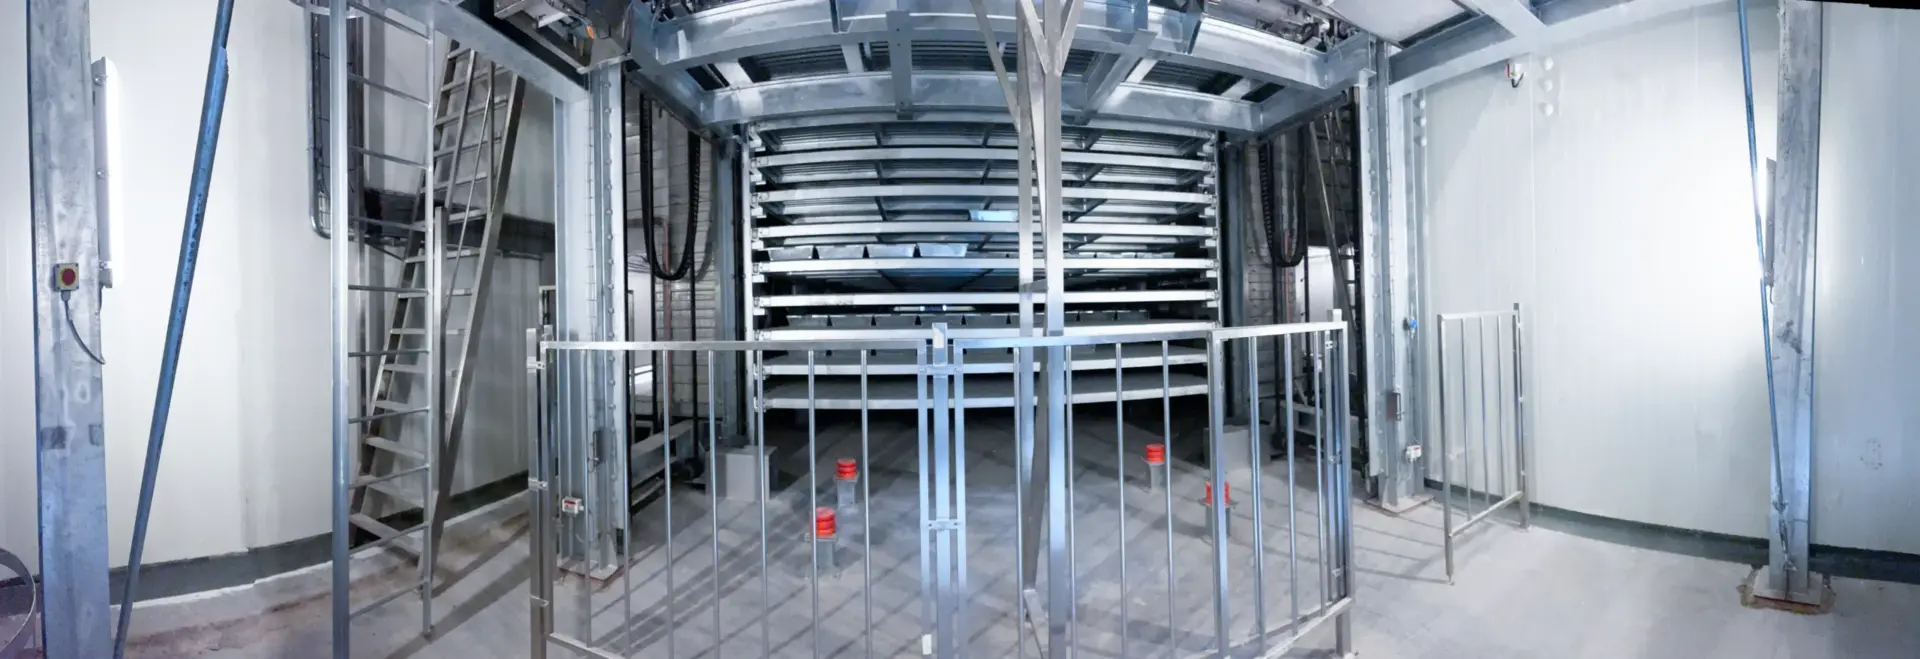
Square’s carton freezer is suitable for freezing beef, poultry, pork, and cooling of fruits, cheese, etc. Our carton freezer efficiently freezes or chills products in cartons, plastic totes, or shrink-wraps. With our tunnel carton freezer, enjoy rapid freezing that optimally preserves your products.
Whether it’s cartons, boxes, trays, or bulk containers, our system ensures quality while reducing labor costs through advanced pre-sorting, freezing units, and output distribution.
Flexible
Smart control
Efficient Horizontal airflow freezing
Low labor intensity
Product tracibilit

Product Features
Explore the key product features, including Efficient Horizontal Airflow Freezing, Low Labor Intensity, Product Traceability, and the engineering advantages behind this system.

Our carton freezer minimizes retention time for boxed products by maintaining consistent air freezing temperature and speed horizontally across all levels.

Reduce workload and time, resulting in decreased labor costs with our carton freezer.

Trace batch numbers, freezing times, and locations of products for enhanced traceability.

Capable of freezing multiple products simultaneously, offering versatility in production.

Equipped with PLC control, servo motor monitoring system, and remote troubleshooting capabilities for efficient and intelligent operation.
Technical Specifications
Carton freezer parameters cover tunnel configuration, conveying layout, airflow, freezing capacity, temperature range, refrigerant, defrost, loading height, controls, and carton handling.
| Configuration | Multi-level conveyorized carton freezer — straight-through or U-shape |
|---|---|
| Capacity | 2 – 15 tons/hr (product and carton size dependent) |
| Carton sizes | 300×200×100 mm to 600×400×200 mm (standard); custom sizes accommodated |
| Conveyor levels | 2 – 6 levels for extended dwell time |
| Operating temperature | −35°C to −40°C (air); −30°C to −35°C (evaporator) |
| Refrigerant | NH₃ (Ammonia) / CO₂ — pump-recirculated |
| Evaporator | Industrial finned-tube, stainless steel or aluminium, multi-bank |
| Defrost | Hot gas / Water — automated, production-continuous with multi-bank design |
| Typical freeze time | 4 – 24 hours (carton size and product dependent) |
| Infeed/Outfeed | Automated conveyor with barcode scanning and palletizing interface |
| Control system | PLC with SCADA, WMS integration, batch traceability, automated reporting |
| Typical lead time | 18–24 weeks |
| Design life | 20+ years (structure); 15+ years (refrigeration); 8–12 years (conveyors) |
Design Details
Expand any section below for the engineering approach behind each critical subsystem — with links to detailed Technology pages.
Carton freezers provide distinct advantages for boxed products:
The material handling system is integral to carton freezer performance:
Freezing time for cartoned product is determined by:
Typical freezing time for a standard 25 kg meat carton from +5°C to −18°C core at −38°C air: 10–16 hours.
Carton freezers handle high product heat loads:
Carton freezers typically sit between production/packing and cold storage:
Freezes boxed meat and poultry products uniformly while protecting carton shape and package integrity.
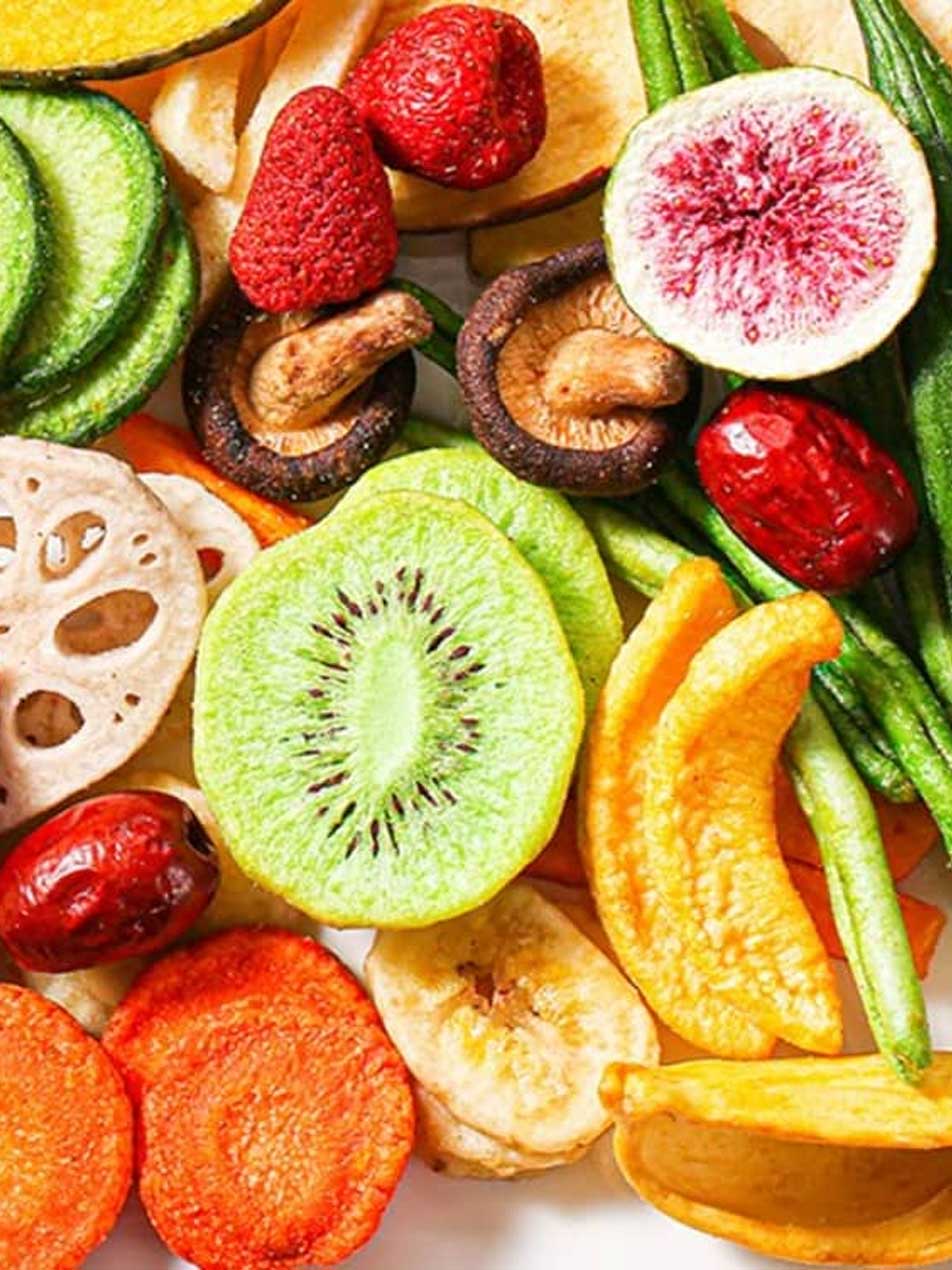
Suitable for packaged fruit products requiring stable temperatures and gentle, even airflow.
Case Studies
Real production lines with performance data — not renderings, not claims. Each installation documented with commissioning data.
No. The freezer is designed with gentle airflow and even cooling to maintain the shape and integrity of the packaging throughout the cycle.
Yes. Most modern Carton Freezers support integration with automatic conveyors, AGVs, and palletizers for efficient material handling.
We own CE, EAC, INF, CNAS, ISO, ASME, PED, U2, CSA, CRN certifications and 300+ patents, as well as 350+ engineers. Square vertically integrated production ensures quality control from raw materials.
Square can customize carton freezer tunnel length, belt width, airflow arrangement, loading height, infeed/outfeed direction, refrigerant, defrost method, and automation interfaces to match carton size, throughput, and plant layout.
Consistent freezing is maintained through controlled airflow, proper spacing, stable conveying, and a refrigeration layout matched to carton size and load density. Square configures the tunnel and airflow according to the product and package format.
Engineering Inquiry
Share your product type, target capacity, line layout, utilities, and site conditions. Our engineers will review your requirements and recommend a suitable Carton Freezer configuration.